The continued global evolution of industrial heating initiatives and heat transfer applications brings with it new challenges – and also new solutions.
In South America, environmental regulations, cost management, natural conditions, and overall efficiency require careful planning and the integration of technology that will adhere to best practices, offer prime efficiency, and foster the greatest return on investment.

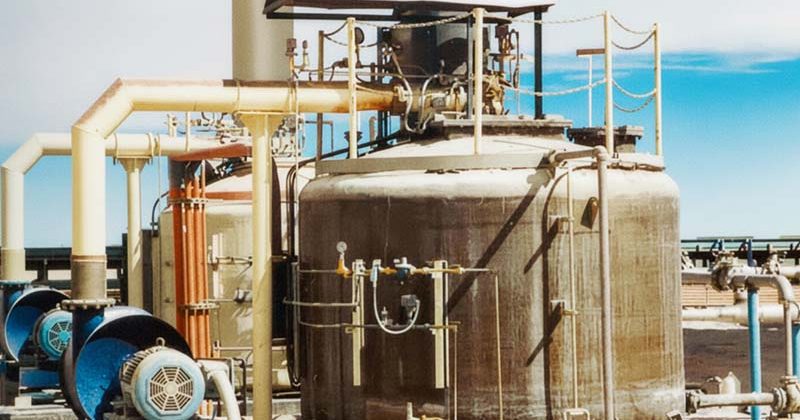
A SubCom®10 MM BTU/hr raffinate solution heater for Compania Minera Cerro Colorado in Iquique, Chile
Submerged Combustion – or SubCom® – direct-fired heaters are a proprietary product from Inproheat Industries. For companies in South America, they can provide cutting-edge thermal efficiency in industrial applications relating to liquid heating and evaporation.
Inproheat has five decades of history with successful SubCom® projects and an international reach that goes far beyond its Canadian headquarters.
Already familiar in the South American market dating back to 1996, Inproheat designed a SubCom® raffinate solution heating system for a copper mine near Iquique, Chile operated by Compania Minera Cerro Colorado, a subsidiary of BHP Billiton Ltd. Inproheat has also participated in Enermin 2016 with the presentation “Efficient Volume Reduction and Concentration of Mining Waste Water with Direct Contact Evaporation Technology”, which focused on the ties between SubCom® and renewable energy and efficiency.

Inproheat President Steve Panz (second from left) on site in Chile.
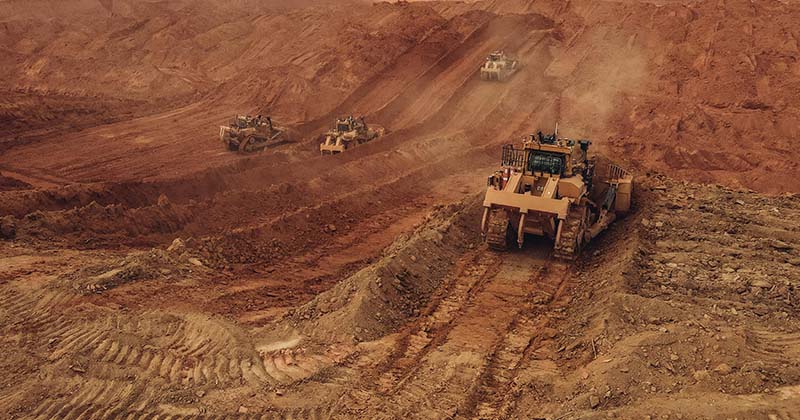
South America remains an international hub with current extraction projects focused primarily on the following minerals:
As it stands now, many forward-thinking mining companies in South America are poised to benefit from what Inproheat and SubCom® direct-fired heaters can offer.

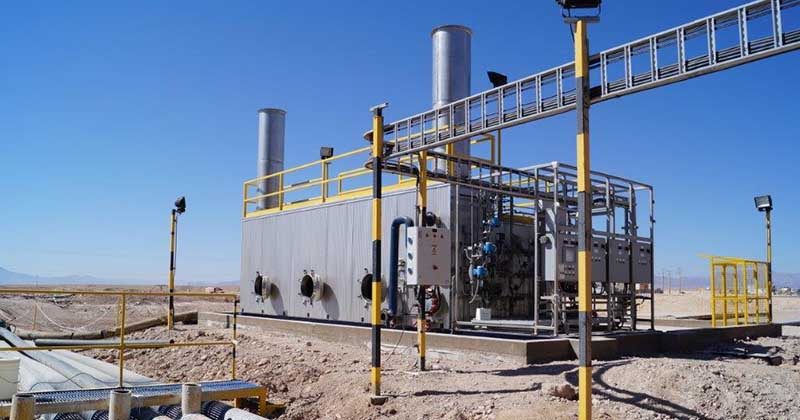
A SubCom® 30 MM Btu/h oil fired brine heater for Atacama Minerals.
For South America-based industrial applications, SubCom® direct-fired heaters for liquid heating and evaporation offer a host of key benefits.
Among them:
Efficiency:
• Up to a 10:1 turndown ratio
• Thermal efficiencies over 99% can be achieved
• 10-15% more efficient than a traditional boiler or heat exchanger system
• Highly adaptive to a wide range of heating
• SubCom® direct fired heaters also have zero loss of efficiency during their lifespans.
Cost Savings:
• Short capital cost recovery compared to conventional heating methods, as well as traditional fluid disposal and recycling methods.
• 10% to 30% in fuel savings.
• No pre-treatment or post-treatment of the solution is required, so no process costs are needed.
Environmentally Responsible:
• The increased efficiency of SubCom® direct-fired heaters results in equivalent reduction in carbon emissions.
• Low NOx burner technology
• Water recovery from the exhaust of a SubCom® direct-fired evaporator can be condensed and recycled for other areas of the process, reducing freshwater usage.
Flexible Design:
• Modular design and construction
• Skid-mounted and semi-transportable versions
Safe and Reliable Operation and Low Maintenance:
• Inherently safe as the combustion process is fully-contained by non-flammable liquid with exhaust gases exiting at near ambient liquid temperature.
• Exhaust temperatures are typically 200°F to 300°F (100°C to 150°C) less than boiler systems.
• Few wearable parts and no heat transfer surfaces to plug, foul or corrode.
• A durable industrial heating solution for challenging South American environments.
• Not a pressure vessel, therefore no regulatory operator certification is required.
• Minimal downtime.
Beyond industrial mining applications, direct-fired evaporators using SubCom® technology for energy-efficient industrial evaporation are relevant to a range of additional industry sectors that are unique to South America.
SubCom® industrial evaporation applications include:
SubCom® direct fired heaters are well-suited in South America to industrial applications by companies in Chile, Peru, and Brazil use direct contact process liquid heating, along with those in search of heat transfer solutions via direct-contact heat exchangers.
SubCom® industrial liquid heating applications include:

In a time of change, Inproheat’s proprietary submerged combustion technology is designed to meet the current and future needs of the industrial heating and evaporation markets throughout South America.
Inproheat’s planned project expansion into South America will focus on the critical markets of Chile, Peru, Brazil, Argentina, Bolivia, and Colombia.
Thermal Engineering Ltda is representing Inproheat in Conchali and Santiago, Chile and is assisting us on select projects in Peru.
We look forward to the opportunity to enhance your South America-based project with the proven benefits that SubCom® has to offer.
Are you interested in learning more about how SubCom® can be integrated into your company’s industrial application in the South American market?
Please complete our information request form to receive a consultation to discuss the ways that Inproheat can assist with your project. One of our representatives will be in touch with further details.
Please allow up to 24 hours for a response during regular business hours.